Welded Pipe Process
Date: 2023-09-08
Welded Pipe Process
Welded Pipe Process
Electric Resistance Welding Process (ERW)
Steel Pipe In the resistance welding process, pipes are produced by hot, and cold forming of a sheet of flat steel in a cylindrical geometry. Electric current then passes through the edges of the steel cylinder to heat the steel and form a bond between the edges to the point where they are forced to meet. During the REG process, filler material may also be used. There are two types of resistance welding: high-frequency welding and rotating contact wheel welding.
The requirement for high-frequency welding stems from the tendency for low-frequency welded products to experience selective joint corrosion, hook cracking, and inadequate joint bonding. Therefore, the explosive remnants of low-frequency warfare are no longer used to make pipes. The high-frequency ERW process is still used in tube manufacturing. There are two types of high-frequency REG processes. High-frequency induction welding and high-frequency contact welding are types of high-frequency welding. In high-frequency induction welding, the welding current is transmitted to the material through a coil. The coil does not come into contact with the pipe. Electric current is generated in the tube material by the magnetic field surrounding the tube. In high-frequency contact welding, electric current is transmitted to the material through contacts on the strip. Welding energy is applied directly to the pipe, making the process more efficient. This method is often preferred for producing pipes with large diameters and high wall thickness.
Another type of resistance welding is the rotating contact wheel welding process. During this process, electric current is transmitted through the contact wheel to the welding point. The contact wheel also creates the pressure needed for welding. Rotary contact welding is typically used for applications that cannot accommodate obstacles inside the pipe.
Electric Fusion Welding Process (EFW)
The electric fusion welding process refers to the electron beam welding of a steel plate using the high-speed motion of the electron beam. The strong impact kinetic energy of the electron beam is converted into heat to heat the workpiece to create a weld seam. The weld area can also be heat treated to make the weld invisible. Welded pipes typically have tighter dimensional tolerances than seamless pipes and, if produced in the same quantities, cost less. Mainly used for welding various steel plates or high energy density welding, metal welded parts can be rapidly heated to high temperatures, melting all refractory metals and alloys .
Submerged Arc Welding Process (SAW)
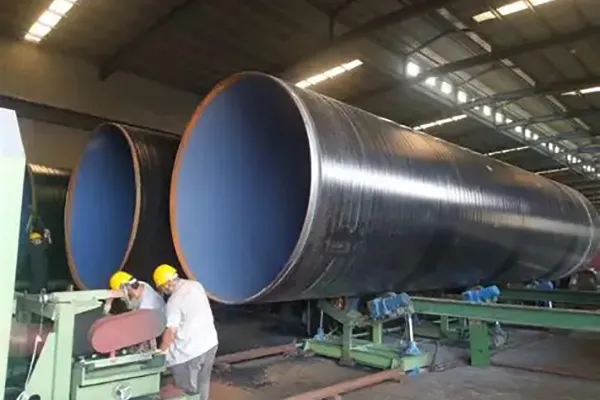
Submerged arc welding involves forming an arc between a wire electrode and the workpiece. A stream is used to generate shielding gas and slag. As the arc moves along the seam, excess flow is removed through a funnel. Because the arc is completely covered by the flux layer, it is usually invisible during welding, and heat loss is also extremely low. There are two types of submerged arc welding processes: vertical submerged arc welding process and spiral submerged arc welding process.
In longitudinal submerged arc welding, longitudinal edges of steel plates are first beveled by milling to form a U shape. Edges of the U-shaped plates are then welded. Pipes manufactured by this process are subjected to expanding operation in order to relieve internal stresses and obtain a perfect dimensional tolerance.
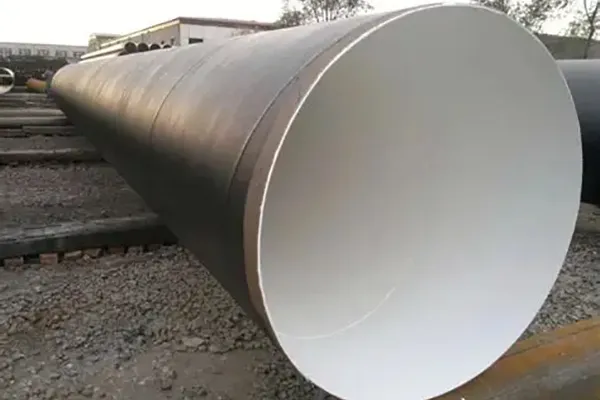
In spiral submerged arc welding, weld seams are like a helix around the pipe. In both of the longitudinal and spiral welding methods the same technology is utilized, the only difference is the spiral shape of seams in spiral welding. The manufacturing process is to roll the steel strip so that the rolling direction forms an angle with the radial direction of the tube, shape, and weld so that the weld line lies in a spiral. The main disadvantage of this process is the poor physical dimensions of the pipe and the higher joint length which can easily lead to the formation of defects or cracks.
Post time: Sep-08-2023





 English
 Español
 русский язык
 Português