Industry News

Hunan Great Steel Pipe Co., Ltd
3PE anti-corrosion steel pipe maintenance,3PE coated steel pipe,3PE pipeline maintenance

How Should 3PE Anti-Corrosion Steel Pipe Be Maintained After Installation

Date: 2026-08-20
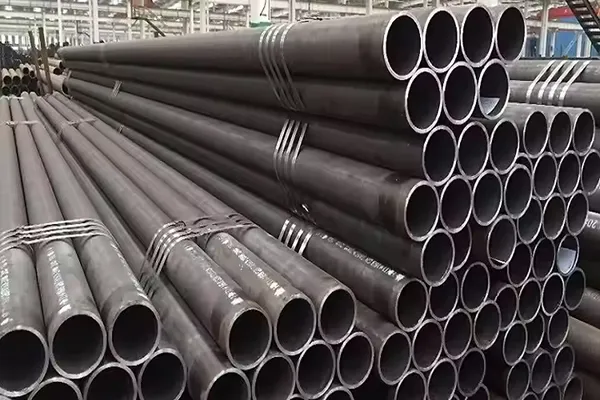
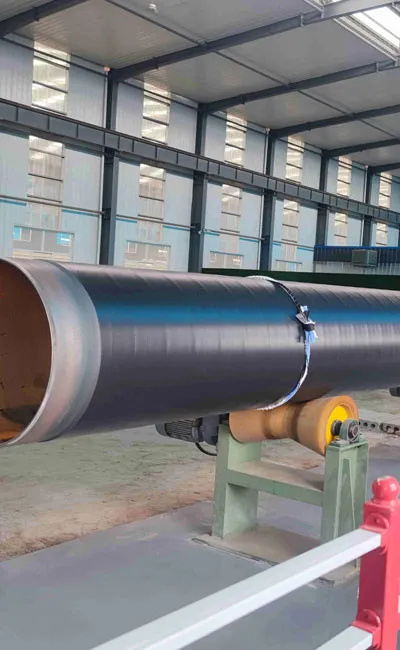
A 3PE anti-corrosion steel pipe does not stop requiring attention once it has been installed and buried. The three-layer polyethylene coating is designed to isolate the steel from moisture, soil, and other corrosive conditions, but the coating can still be damaged during transportation, welding, backfilling, excavation, or pipeline operation. ISO 21809-1:2018 specifies requirements for plant-applied three-layer polyethylene and polypropylene coatings used to protect buried or submerged steel pipelines. It also recognizes that these coated pipes can be used with cathodic protection. For this reason, post-installation maintenance should focus on the complete corrosion protection system rather than the polyethylene layer alone.

1. What Should Be Checked After Installation?

The first inspection should confirm that the coating has not been compromised during construction. Although 3PE coating is normally applied under controlled factory conditions, handling and installation introduce different risks. Lifting equipment, pipe supports, welding operations, rocks in the trench, and backfilling can cause cuts, gouges, holidays, or local disbondment. Before final acceptance or commissioning, inspection should pay particular attention to: 
  • Exposed sections of coated pipe
  • Coating transition areas
  • Field joints
  • Valve and fitting connections
  • Road and river crossings
  • Locations affected by construction equipment
Where required by the project specification, electrical holiday detection can help identify coating discontinuities that cannot be reliably identified by visual inspection alone. Pipeline projects may also specify inspection of coating thickness, application quality, and field-joint coating before backfilling.

2. How Can Mechanical Damage Be Prevented?

Once the pipeline is buried, unnecessary excavation near the pipe should be avoided. Future construction, foundation work, road expansion, or agricultural activities can expose the pipeline to mechanical damage. If excavation is necessary, the pipeline location should be established before mechanical equipment is used. After exposure, the coating should be protected from sharp tools, dragging, impact, and uncontrolled contact with rocks. Backfill material also matters. Large or sharp stones directly against the coating can create localized mechanical stress. The project specification should therefore define suitable padding and backfilling practices for the pipeline environment.

3. Why Are Field Joints Critical?

The factory-applied 3PE coating does not cover the girth weld area between two pipe sections. The field joint must therefore be protected separately after welding. This creates an important transition between factory coating and field-applied coating. Unlike factory production, field joint application takes place under changing site conditions, making surface preparation, heating, coating application, and inspection especially important. Industry literature has long identified field-applied joint protection as a critical part of maintaining continuous pipeline corrosion protection. During maintenance, operators should look for:
  • Cracking or lifting around the joint
  • Disbondment
  • Water ingress
  • Mechanical damage
  • Poor overlap with the mainline coating
  • Evidence of corrosion near the joint
A damaged field joint should be repaired using the approved repair system rather than simply covered with an unrelated coating material.

4. How Should Cathodic Protection Be Monitored?

3PE coating provides passive corrosion protection, while cathodic protection can provide additional protection at coating defects or exposed steel. ISO 21809-1 specifically notes the suitability of coated pipe for further protection by cathodic protection. Maintenance should therefore include monitoring of the cathodic protection system according to the applicable design and regulatory requirements. Typical checks may include:
  • Pipe-to-soil potential
  • Rectifier performance
  • Anode condition
  • Electrical continuity
  • Insulating joint performance
  • Changes in cathodic protection current demand
A change in CP performance can sometimes indicate a developing coating problem. It should therefore be evaluated together with coating inspection results rather than treated as an isolated electrical measurement.
5. When Does a 3PE Coating Need Repair?

Not every surface mark requires the same repair procedure. The decision should consider the location, size, depth, and extent of the damage. Repair should generally be considered when:
  • The steel substrate is exposed
  • A coating holiday is detected
  • The coating has been cut, gouged, or torn
  • Significant disbondment is found
  • Water has entered beneath the coating
  • Field-joint protection has deteriorated
  • Inspection results indicate a potential path for external corrosion
The repair area should be properly prepared, repaired with a compatible system, and inspected again before the pipeline is returned to service or the excavation is closed.

6. How Should Maintenance Records Be Managed?

A reliable maintenance program should leave a clear record of what was inspected and what changed over time. Records should include the pipeline section, inspection date, coating condition, detected defects, repair method, cathodic protection measurements, and follow-up results. Keeping this information together allows operators to compare current conditions with previous inspections and identify recurring problem areas.

Conclusion

Maintaining a 3PE anti-corrosion steel pipe is not simply a matter of checking whether the polyethylene surface still looks intact. Long-term corrosion protection depends on the condition of the coating, field joints, cathodic protection system, surrounding environment, and repair history. The practical approach is straightforward: inspect after installation, prevent mechanical damage, control field joints, monitor cathodic protection, repair coating defects promptly, and keep complete records. For pipeline projects, these controls should be established before installation and aligned with the applicable coating standard, project specification, operating conditions, and corrosion-control design. This makes 3PE protection part of a long-term pipeline integrity strategy rather than a one-time coating treatment.

Latest news list

  • alloy steel pipe buying guide,buy alloy steel pipe,alloy steel pipe supplier,alloy steel pipe export
    Buying alloy steel pipe for an international project involves more than comparing prices per tonne,For EPC contractors,distributors and industrial buyers,procurement needs to connect technical specifications,quality control,inspection,documentation and logistics,A well-defined purchasing process helps reduce specification gaps,inspection delays and delivery problems before the pipe reaches the project site,
  • how to select alloy steel pipe,alloy steel pipe selection,alloy steel pipe buying guide,high temperature alloy steel pipe
    Selecting alloy steel pipe should start with the actual service conditions,not simply with a supplier's product catalog,In boiler,power generation and refinery applications,temperature,pressure,process medium and material properties all affect pipe selection,For example,ASTM A335,A335M-26 covers seamless ferritic alloy-steel pipe for high-temperature service,The standard states that selection depends on design,service conditions,mechanical properties and high-temperature characteristics,For buyers,a structured selection process helps prevent specification gaps before production begins,
  • alloy steel pipe maintenance,alloy steel pipe boiler usage,alloy steel pipe refinery,high temperature pipe maintenance
    Alloy steel pipe is widely used in boiler,power generation and refinery systems where piping is exposed to elevated temperatures,pressure and demanding process conditions,Selecting the correct alloy grade is important,but material selection alone does not determine service life,Long-term performance also depends on operating conditions,thermal exposure,wall thickness,fabrication quality,inspection and maintenance,For example,ASTM A335,A335M-26 covers seamless ferritic alloy-steel pipe for high-temperature service and states that material selection depends on design,service conditions,mechanical properties and high-temperature characteristics,
  • alloy steel pipe quality control,alloy steel pipe inspection,alloy steel pipe mechanical properties
    For alloy steel pipe used in boilers,power plants,refineries and other demanding industrial systems,quality control should cover the complete supply chain from raw material identification to final shipment,A pipe can meet the required outside diameter and wall thickness and still fail to satisfy the project specification if the material grade,heat treatment,mechanical properties or inspection records are incorrect,For buyers,effective quality control means verifying both the physical product and the evidence behind it,
  • alloy steel pipe high temperature,alloy steel pipe applications,alloy steel pipe selection,alloy steel pipe
    High-temperature process piping places demanding requirements on pipe materials,As temperature increases,material strength can change,oxidation can become more significant,and long-term exposure can affect the service condition of the piping system,Alloy steel pipe is commonly selected for applications where elevated-temperature mechanical performance is required,Typical uses include refinery process lines,petrochemical units,boiler and steam systems,power-generation facilities and other industrial piping operating under elevated temperature and pressure,The correct selection,however,depends on the complete service condition rather than temperature alone,

Find what you need ?

close
We use cookies and other tracking technologies to improve your browsing experience on our website, to show you personalized content and targeted ads, to analyze our website traffic, and to understand where our visitors are coming from.