Quality control is one of the most important factors affecting the performance of
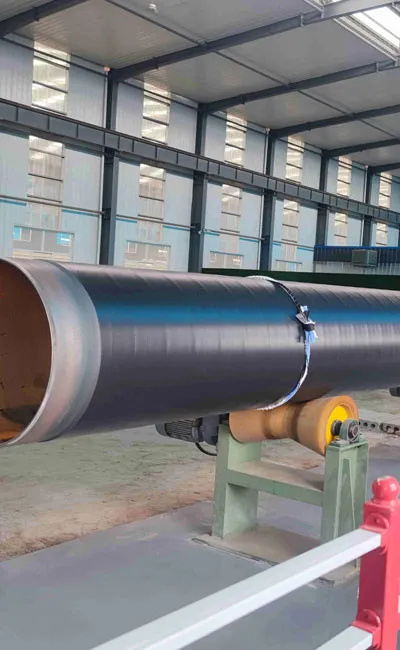
3PE anti-corrosion steel pipe. A three-layer coating can provide effective external protection only when the steel surface, coating materials, application process, inspection, and subsequent handling are properly controlled. A typical 3PE system consists of fusion-bonded epoxy (FBE), copolymer adhesive, and polyethylene (PE). ISO 21809-1:2018 specifies requirements for plant-applied three-layer PE and PP external coatings for welded and seamless steel pipe used in petroleum and natural gas pipeline transportation systems. The standard covers buried or submerged pipeline applications and notes that coated pipes are suitable for further protection by cathodic protection. For buyers and EPC contractors, the important point is that 3PE quality should not be judged by the final appearance alone. Reliable QC starts before coating and continues through inspection, repair, handling, and release.
What Does 3PE Quality Control Include?
A practical quality-control sequence is: Base Pipe Inspection → Surface Preparation → FBE Application → Adhesive & PE Application → Final Inspection → Repair → Documentation → Release. Each stage creates evidence for the next stage and helps prevent defects from being carried forward.
1. Inspect the Steel Pipe Before Coating
The coating process starts with the condition of the steel pipe. Typical checks may include:
-
Steel grade and pipe standard
-
Outside diameter and wall thickness
-
Pipe length
-
Surface condition
-
Weld condition for welded pipe
-
Identification and traceability
The coating should not be regarded as a way to cover defects in the base pipe. Any condition that could affect coating integrity should be identified before surface preparation and coating.
2. Control Surface Preparation
Surface preparation is a critical stage of 3PE quality control. Before FBE application, the steel surface must be prepared according to the approved specification. AMPP notes that pipeline surface preparation is normally specified by the asset owner with input from the coating manufacturer, and that blast-cleaning requirements are commonly defined by applicable standards. QC personnel may verify:
-
Surface cleanliness
-
Surface profile
-
Dust or other contamination
-
Residual rust or mill scale
-
Surface temperature
-
Environmental conditions
This step deserves particular attention because inadequate cleaning or an unsuitable surface profile can reduce adhesion and contribute to premature coating problems. AMPP's FBE guidance identifies surface cleanliness and profile as important inspection considerations.
3. Control FBE Application
The FBE layer is applied directly to the prepared steel and forms an important corrosion-protection component of a typical 3PE system. Depending on the approved procedure, QC may monitor:
-
Substrate preheating
-
FBE material condition
-
Application parameters
-
Coating thickness
-
Cure condition
-
Surface appearance
The actual process limits should come from the coating manufacturer's technical data and project specification. AMPP notes that incorrect preheating, poor powder application, and incomplete curing can affect FBE performance. Inspection may include thickness measurement, visual examination, cure verification, adhesion testing, or other specified tests.
4. Inspect the Adhesive and PE Layers
After FBE, the copolymer adhesive and polyethylene outer layer are applied. Quality control focuses on whether the layers are correctly applied and properly integrated into the coating system. Depending on the project requirements, checks may include:
-
Coating material identification
-
Application temperature
-
Layer bonding
-
Coating thickness
-
Surface appearance
-
Visible defects
The objective is not simply to confirm that three materials are present. The three layers must function together as one continuous protective system.
5. Check Coating Thickness and Continuity
Final inspection should combine visual examination with appropriate measurement methods. Typical checks may include:
-
Visual inspection: Identifies exposed steel, scratches, wrinkles, bubbles, impact damage, and other visible defects.
-
Coating thickness measurement: Confirms that the finished coating falls within the specified range.
-
Holiday or discontinuity detection: Identifies pinholes or other discontinuities that may not be visible to the naked eye. AMPP maintains dedicated inspection guidance for discontinuity testing of protective coatings on conductive substrates.
The inspection method, testing voltage, frequency, and acceptance criteria should always follow the applicable standard and project specification rather than using one universal value.
6. Repair and Reinspect Coating Defects
When a coating defect is identified, it should be repaired using an approved procedure and compatible repair material. A practical repair sequence is:
Identify Defect → Prepare Surface → Apply Approved Repair → Reinspect → Record. The repaired area should be checked again using the inspection methods required by the project. This closed-loop approach is important because a repair that looks acceptable visually may still require thickness, continuity, adhesion, or other verification.
7. Maintain Quality After Factory Coating
One of the most overlooked parts of coated pipe quality is what happens after the coating line. The practical supply chain is:
Coating → Transportation → Storage → Lifting → Field Welding → Installation. Rough handling or unsuitable lifting can damage the PE outer layer. Field welding also creates areas where the factory coating is removed and must subsequently be protected with an appropriate field-joint coating system. AMPP notes that pipeline sections are commonly left uncoated at their ends to allow field welding, after which the joint area requires separate coating treatment. Therefore, a complete QC approach should consider transportation, storage, handling, field-joint requirements, and installation—not just factory inspection.





 English
 Español
 русский язык
 Português