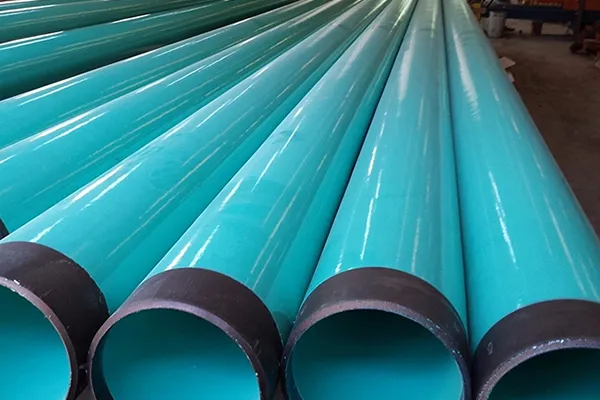
Selecting an external coating for buried steel pipe is not simply a matter of choosing more coating layers. The right system depends on soil conditions, operating requirements, installation methods, mechanical exposure, applicable standards, and the level of corrosion protection required. 2PE and 3PE are both polyethylene-based external coating systems, but their structures are different. Understanding that difference helps EPC contractors, distributors, and pipeline operators make a more informed purchasing decision.
What Is the Structural Difference Between 2PE and 3PE?
A typical 2PE system consists of an adhesive layer and a polyethylene outer layer:
2PE: Steel → Adhesive → Polyethylene
A typical 3PE system adds a fusion-bonded epoxy (FBE) primer:
3PE: Steel → FBE → Adhesive → Polyethylene
The FBE layer is the primary structural difference. In 3PE coating, FBE is applied directly to properly prepared steel. The adhesive layer bonds the epoxy to the polyethylene outer layer, while the PE layer provides additional protection against moisture, soil exposure, abrasion, and mechanical damage. The exact coating structure, thickness, and acceptance criteria should always follow the applicable project specification. ISO 21809-1:2018 specifies requirements for plant-applied three-layer polyethylene and polypropylene external coatings for welded and seamless steel pipe used in petroleum and natural gas pipeline transportation systems. The standard is currently published and is under revision.
What Does the FBE Layer Add?
The main reason for adding FBE is to provide a dedicated epoxy layer directly on the prepared steel surface. A typical 3PE system therefore combines three functions:
-
FBE: Corrosion protection and adhesion to the steel substrate
-
Adhesive: Bonding between FBE and polyethylene
-
PE: Mechanical and environmental protection
This multilayer structure allows different coating materials to perform different jobs rather than requiring one material to provide every type of protection. For buried pipelines, that distinction matters because the external steel surface becomes difficult to access after backfilling. Coating quality therefore needs to be considered before installation, not only when maintenance problems appear.
When Can 2PE Be Considered?
2PE should not automatically be viewed as an inferior version of 3PE. A two-layer system may be considered when:
-
The project specification permits 2PE.
-
The service environment is compatible with the specified coating.
-
The required corrosion and mechanical protection can be achieved with the selected system.
-
The pipeline does not require an FBE primer under the applicable specification.
-
The overall project requirements favor a simpler coating structure.
The decision should be based on engineering requirements rather than coating terminology alone. For example, a pipeline operating in a relatively moderate external environment may have different coating requirements from a buried pipeline exposed to high soil moisture, salts, or other aggressive conditions.
3PE may be considered when the project requires a multilayer system combining an epoxy corrosion barrier with a polyethylene outer layer. Typical considerations include:
-
Buried or submerged pipeline applications
-
More demanding external corrosion environments
-
Requirements for strong adhesion to the prepared steel surface
-
Combined corrosion and mechanical protection
-
Project specifications that specifically require 3PE
ISO 21809-1:2018 covers three-layer PE and PP external coatings for buried or submerged pipeline systems and notes that pipes coated in accordance with the standard are considered suitable for further protection by cathodic protection. This does not mean that every buried pipeline requires 3PE. The final coating selection should follow the approved engineering specification.
What About Cost?
Cost is an important procurement consideration, but it should not be reduced to the statement that “2PE is cheaper.” A typical 2PE system has fewer coating components, while 3PE includes an additional FBE layer and associated application and inspection requirements. The final price can vary with:
-
Pipe diameter and wall thickness.
-
Coating thickness
-
Order quantity
-
Raw material costs
-
Inspection requirements
-
Coating class
-
Transportation and handling conditions
For long-term pipeline assets, buyers should also consider installation, repair, inspection, and potential maintenance requirements rather than comparing coating prices alone.
What Happens After the Coating Plant?
Coating performance depends on more than factory application. A practical supply chain is:
Factory coating → Transportation → Storage → Lifting → Field welding → Installation
Damage can occur during handling, lifting, transportation, or trench installation. Field welding also creates areas where the original factory coating has been removed and must be restored. ISO 21809-3:2016 specifically addresses field-joint coating for buried and submerged pipeline systems, including qualification, application, and testing of coatings applied to steel surfaces left exposed after welding. From a supply perspective, this means coating requirements should be reviewed together with transportation, storage, field-joint treatment, installation, and repair procedures.
What Should Be Included in a 2PE or 3PE RFQ?
A clear RFQ should define:
-
Pipe standard and steel grade
-
Outside diameter and wall thickness
-
2PE or 3PE coating requirement
-
Coating class and thickness
-
Operating temperature
-
Soil and installation environment
-
Field-joint coating requirements
-
Inspection and testing requirements
-
Quantity and delivery conditions
Providing this information allows the manufacturer to evaluate the steel pipe and coating system as one complete project requirement.
Conclusion
The main difference between 2PE and
3PE coated steel pipe is the FBE primer. A typical 2PE system uses adhesive and polyethylene, while a typical 3PE system adds FBE between the steel substrate and adhesive. 3PE may be preferred where a dedicated epoxy corrosion barrier and multilayer protection system are required, while 2PE can be considered when a simpler coating system satisfies the project specification. The right choice should ultimately be based on service environment, operating conditions, mechanical exposure, installation method, applicable standards, coating requirements, and total project cost. For EPC contractors, distributors, and industrial buyers, defining these requirements before production helps ensure that the selected coating system is appropriate for the actual pipeline conditions. Need help selecting 2PE or 3PE
coated steel pipe for your project? Contact our technical team with your pipe specifications, service conditions, and coating requirements for a project-specific evaluation.








 English
 Español
 русский язык
 Português












