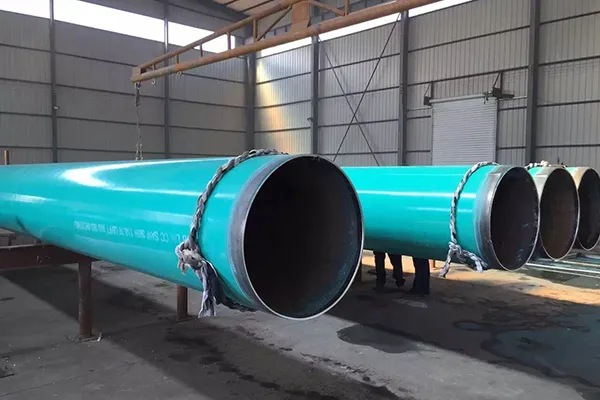
5. Adhesion, Curing and Other Performance Tests
FBE is a heat-activated thermosetting epoxy coating. Its final performance depends on appropriate application and curing conditions. Depending on the coating specification and qualification requirements, testing may include:
-
Degree of cure
-
Adhesion
-
Impact resistance
-
Flexibility
-
Cathodic disbondment resistance
These tests do not necessarily apply to every production pipe. Some are used during coating system qualification or procedure approval, while others may be required for production testing or specific project acceptance. The test method, sampling frequency and acceptance criteria should be agreed in the applicable specification and ITP.
6. Documentation and Traceability
Inspection results are useful only when they can be linked to the actual supplied pipe. A project quality package may include:
-
Bare pipe material certificates
-
FBE powder batch information
-
Application Procedure Specification (APS)
-
Inspection and Testing Plan (ITP)
-
Surface preparation and coating application records
-
Thickness and holiday detection reports
-
Applicable performance test results
-
Repair and retest records
-
Final inspection and traceability records
The APS defines the approved coating application procedure, while the ITP identifies inspection stages, test methods, frequencies and acceptance criteria. For oil and gas pipeline applications, ISO 21809-2:2026 provides requirements for plant-applied single-layer external FBE coatings. For steel water pipe and fittings, ANSI/AWWA C213-22 is a relevant reference. Their application scopes are different, so buyers should specify the appropriate standard and edition.
What Should Buyers Include in an FBE Coating Inspection Plan?
Avoid using a general requirement such as "FBE coating to international standard" without defining the actual acceptance requirements. Before ordering, buyers should confirm the applicable standard and edition, coating class, minimum and maximum thickness, pipe-end cutback, inspection methods, test frequency, repair procedures and documentation requirements.
At Hunan Great Steel Pipe Co., Ltd., we coordinate inspection requirements with relevant supply and coating parties according to confirmed project specifications. This includes production progress coordination, factory inspection arrangements and quality documentation review.
FAQ
Q1. What are the main inspection methods for FBE coated steel pipes?
A1. Common checks include visual inspection, surface preparation assessment, coating thickness measurement and holiday detection. Adhesion, curing and other performance tests may also be required.
Q2. What is a holiday in FBE coating?
A2. A holiday is a discontinuity in the coating that may expose the steel substrate. It is generally identified through an electrical continuity test.
Q3. Does holiday detection confirm the overall quality of an FBE coating?
A3. No. It checks coating continuity but does not verify adhesion, curing or mechanical performance. These properties require separate inspections or tests where specified.
Q4. Is coating thickness the only factor that determines FBE quality?
A4. No. Surface preparation, coating application, curing, adhesion, coating continuity and repair quality all contribute to the final result.
Q5. Does every FBE coated pipe require the same inspection tests?
A5. No. Requirements depend on the applicable standard, coating system, project specification and approved ITP. Qualification tests and routine production inspections may also have different requirements.





 English
 Español
 русский язык
 Português