Product News

Hunan Great Steel Pipe Co., Ltd
Hydraulic Steel Pipe Quality Control,Hydraulic Tube Inspection,EN 10305-1 E355,Hydraulic Cylinder Tube

How Is Hydraulic Steel Pipe Quality Controlled? A Complete Guide from Raw Material to Final Inspection

Date: 2026-07-30
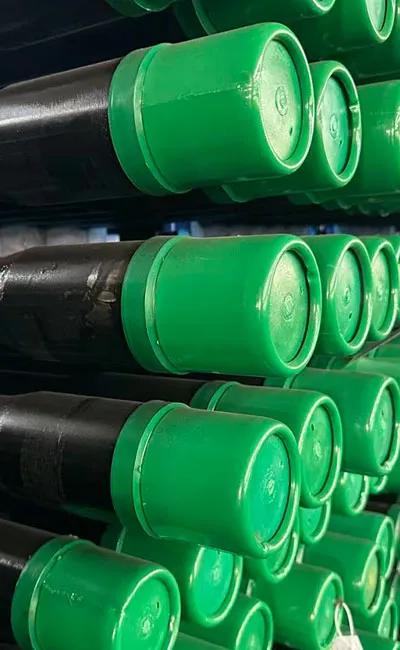
Hydraulic steel pipe quality control is a closed-loop process that starts with raw material verification and follows every tube through cold drawing, heat treatment, dimensional gauging, non-destructive testing, and final documentation review. This systematic approach ensures the finished tube can handle real-world pressure spikes without failure. Here’s how it works, and what buyers should verify before placing an order.

Why Quality Control Matters for Hydraulic Steel Pipes

A hydraulic system is only as reliable as its weakest component. If a pipe fails quality control—or bypasses it entirely—the consequences go far beyond a leaking tube. Undetected flaws often trigger hydraulic fluid contamination, pressure drops that stall heavy machinery, and cylinder scoring that costs thousands in unplanned downtime. Rigorous quality control is the only defense against inflated maintenance budgets and safety risks on the shop floor.

Step 1: Raw Material Inspection

Quality control begins before the steel enters the draw bench. We verify every incoming billet against its EN 10204 certificate using optical emission spectrometry (OES) to confirm limits for carbon, manganese, and sulfur—catching off-spec material before it reaches production. Surface checks detect cracks or laps that would worsen during cold working, and each heat number is logged to ensure full traceability from melt to delivery.

Inspection Item

Purpose

Chemical Analysis (OES)

Verify steel grade and element compliance

Visual Surface Check

Detect billets with cracks or seams

Material Certificate Review

Establish full traceability from melt to delivery

Step 2: Manufacturing Process Control

The cold drawing process is where dimensional precision is forged. During drawing, the tube is pulled through a die and over a mandrel, reducing its diameter and wall thickness while refining its grain structure. This cold working increases tensile strength by 20–30%, but it also introduces internal stress—which is why controlled heat treatment (normalizing or stress-relief annealing) follows immediately to restore ductility and prevent cracking. Straightening and cutting are carefully calibrated; even a 0.5mm deviation in straightness can cause misalignment in cylinder assemblies. Every parameter here directly affects the final tolerance and sealing ability.

Step 3: Dimensional Inspection

After cutting, each tube undergoes rigorous dimensional measurement. We check outside diameter (OD) using laser micrometers, wall thickness via ultrasonic gauging, and length to meet exact cutting tolerances. Straightness is verified on granite surface plates, and ovality is measured to ensure roundness for seal compatibility. For hydraulic cylinder applications, maintaining an OD tolerance of ±0.05mm is often non-negotiable—anything looser invites fluid bypass and piston wear.

Parameter

Inspection Purpose

Outside Diameter (OD)

Ensures proper fit in cylinder blocks and fittings

Wall Thickness (WT)

Determines burst pressure rating and safety margin

Straightness

Prevents assembly stress and uneven seal loading

Step 4: Mechanical Property Testing

We cut test pieces from each batch to evaluate yield strength, tensile strength, elongation, and hardness. For an E355 tube, the minimum yield strength must hit 355 MPa, with tensile values ranging from 490 to 630 MPa. Elongation is equally critical—it tells us how much the steel can deform before fracturing. If yield strength falls short, the pipe could permanently deform under pressure; if hardness is too high, it might become brittle and crack under shock loads. These mechanical properties are the bedrock of hydraulic safety.

Step 5: Non-Destructive Testing (NDT)

NDT is where hidden flaws are weeded out. Eddy current testing (ECT) scans the external and internal surfaces for fine cracks, pinholes, and laps. For deeper volumetric defects, ultrasonic testing (UT) sends sound waves through the tube wall to detect inclusions or laminations. Hydrostatic testing—filling the tube with pressurized water—is the final proof test, typically carried out at 1.5 times the working pressure (though some mobile equipment specs demand 1.6x, we always confirm against the drawing). Critical safety applications also undergo full UT scanning alongside standard ECT and hydrostatic checks.

Step 6: Surface Finish and Cleanliness Inspection

This step is often overlooked by generic suppliers, but it's crucial for system longevity. We inspect internal surface roughness using profilometers; for precision hydraulic tubes, we aim for Ra ≤ 0.4μm. Internal cleanliness is verified by flushing with filtered solvent and inspecting residual particles against ISO 4406 standards. Deburring removes sharp edges that could damage seals during assembly, and final rust prevention (VCI paper or oil coating) is applied before packaging. Contamination is the leading cause of valve sticking and pump wear—clean tubes protect those expensive components.
Quality Documents Buyers Should Request

Don’t rely on verbal assurances. Here's a checklist of documents that validate quality:

Document

What It Provides

EN 10204 3.1 Mill Certificate

Confirms chemical and mechanical results traceable to the heat

Dimensional Inspection Report

Lists actual OD, WT, straightness, and length measurements

NDT Report

Details which tests were done (ECT, UT) and acceptable thresholds

Hydrostatic Test Record

Verifies leak-proof performance under pressure

Traceability Number

Links the finished tubes back to the original raw material heat

Common Quality Problems and How to Prevent Them

Even with rigorous controls, deviations can occur. Here's what we watch for and how we prevent them:
  • Surface scratches → Caused by die wear or material handling. Prevention: regular die replacement and protective packing.
  • Wall thickness deviation → Due to uneven drawing or poor mandrel positioning. Prevention: real-time laser gauging during drawing.
  • Rust formation → Storage in high-humidity conditions. Prevention: immediate application of anti-rust oil and indoor warehousing.
  • Poor straightness → Improper straightening roller settings. Prevention: periodic straightness audits using precision measuring tools.

How Buyers Can Evaluate a Hydraulic Steel Pipe Supplier

Before committing, audit the supplier's in-house testing capability—do they operate their own UT unit and spectrometer, or do they outsource everything? Review their warehouse; tubes stored on muddy ground will arrive rusted and contaminated. Examine their traceability workflow: can they produce a single file linking the final tube back to the original billet heat? A supplier who can confidently walk you through each control stage—from raw material to packaging—without generic brochures is usually the one you can trust for long-term reliability.

FAQ

Q1: What inspections are required for hydraulic steel pipes?
A1: At a minimum, chemical analysis, tensile testing, dimensional checks, eddy current testing, and hydrostatic testing should be performed. Critical applications may also require ultrasonic testing.
Q2: What is EN 10204 3.1?
A2: It's a mill inspection certificate where the manufacturer declares that their test results comply with the standard, and the tests were performed by in-house personnel independent of the production team.
Q3: Is hydrostatic testing always required?
A3: Not always, but it is highly recommended for high-pressure or safety-critical systems. It provides undeniable proof of the tube's burst integrity.
Q4: How is dimensional accuracy measured?
A4: Using calibrated instruments like laser micrometers for OD, ultrasonic wall thickness gauges, and straightness measurement tables. Measurements are taken from both ends and the middle of each tube.
Q5: Why is internal cleanliness important?
A5: Even microscopic particles can cause hydraulic valves to stick, accelerate pump wear, and degrade the fluid. Clean tubes directly extend the service life of the entire hydraulic circuit.

Conclusion

Quality control for hydraulic steel pipes is not a single step—it's a comprehensive cycle that spans chemistry, cold forming, heat treatment, metrology, and non-destructive flaw detection. Each stage builds on the previous one to deliver a tube that performs reliably under extreme pressures. Without this rigorous chain, you're not just buying a pipe—you're accepting a risk to your equipment's uptime and safety. If you're sourcing hydraulic steel pipes for cylinders, heavy equipment, or industrial machinery, consult a supplier who can demonstrate each of these control stages. Our engineering team regularly assists clients in matching inspection levels to application risk—reach out if you need tailored specification advice or would like to request a sample test report before your next order.

Latest news list

  • 3PE coated steel pipe maintenance,3PE coating repair,pipeline corrosion protection,buried pipeline maintenance
    3PE anti corrosion steel pipe is designed to reduce external corrosion risk,particularly in buried and submerged pipeline applications,However,a high-quality factory-applied coating does not remove the need for inspection,monitoring,and maintenance after installation,Pipeline conditions can change over time,Coating damage may also occur during installation,excavation,third-party activities,or other maintenance work,A preventive maintenance program helps operators identify potential problems before they develop into more serious pipeline integrity issues,
  • 3PE anti corrosion steel pipe,3PE coated steel pipe,3PE steel pipe selection,3PE coating specification
    Choosing the right 3PE anti corrosion steel pipe is not simply a matter of selecting a pipe with a polyethylene outer layer,For buried pipelines,water transmission systems,oil and gas transportation,and industrial infrastructure,the pipe and coating system need to match the operating environment,installation conditions,technical specification,and inspection requirements,A clear selection process helps buyers reduce coating-related risks before the pipe reaches the jobsite,
  • 3PE anti corrosion steel pipe,3PE coated steel pipe,pipeline corrosion protection,3PE coating layer
    External corrosion is an important consideration for steel pipelines exposed to soil,moisture,salts,groundwater,and other aggressive conditions,For long-distance and buried pipelines,corrosion protection should not be treated as a maintenance issue alone,It needs to be considered from pipeline design and procurement through coating application,installation,and operation,3PE anti corrosion steel pipe provides a multilayer external barrier that helps reduce the steel surface's exposure to the surrounding environment,However,its effectiveness depends on coating quality,installation practices,field joint protection,and the overall corrosion-control strategy,
  • 3PE anti corrosion steel pipe,3PE coating quality control,3PE coating inspection,3PE steel pipe quality
    3PE anti corrosion steel pipe is widely used for buried and submerged pipeline systems because its external coating helps protect the steel substrate from moisture,soil,and other external corrosion risks,However,a good-looking coating does not necessarily mean a qualified coating system,Surface preparation,coating thickness,adhesion,continuity,pipe-end condition,repair,and documentation all need to be controlled,For this reason,3PE quality control should cover the complete production and inspection process rather than relying on final visual appearance alone,
  • 3PE anti corrosion steel pipe,3PE coated steel pipe,3PE coating,3PE steel pipe application
    Buried steel pipelines operate in an environment that is difficult to control,After installation,the pipe may remain in contact with soil,moisture,groundwater,salts,and other external conditions for many years,Without suitable external corrosion protection,the exposed steel surface can gradually deteriorate,This is why 3PE anti corrosion steel pipe is widely considered for buried pipeline systems,Its three-layer external coating creates a protective barrier between the steel surface and the surrounding environment while also providing additional mechanical protection during handling and installation,

Find what you need ?

close
We use cookies and other tracking technologies to improve your browsing experience on our website, to show you personalized content and targeted ads, to analyze our website traffic, and to understand where our visitors are coming from.