Industry News

Hunan Great Steel Pipe Co., Ltd
how to inspect coated steel pipe,coated steel pipe inspection,coated steel pipe quality control

How to Inspect Coated Steel Pipe: A Practical QA/QC Guide

Date: 2026-08-11

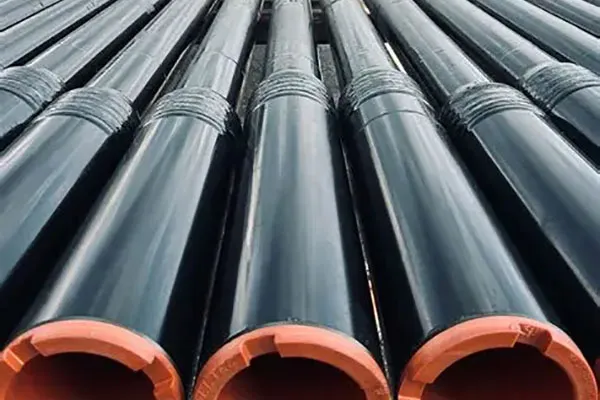
A coated steel pipe should not be accepted simply because its surface looks smooth and uniform. Proper inspection needs to cover both the steel pipe and the protective coating system, from raw material verification through final packaging. For oil and gas pipelines, water transmission systems, industrial piping, and infrastructure projects, coating defects can expose steel to moisture and corrosive environments. A practical inspection process therefore checks the base pipe, surface preparation, coating application, thickness, continuity, documentation, and handling. The exact acceptance criteria should always follow the approved purchase specification, inspection and test plan (ITP), coating manufacturer’s requirements, and applicable standards.


What Should Be Checked on Coated Steel Pipe?

A typical inspection sequence is: Base pipe → Surface preparation → Coating application → Thickness → Defect testing → Documentation → Packaging. Each stage addresses a different potential source of failure.


1. Inspect the Base Steel Pipe

Before checking the coating, confirm that the underlying pipe matches the purchase specification.
Inspectors should verify:

  • Steel grade
  • Outside diameter and wall thickness
  • Pipe length
  • Manufacturing method
  • Dimensional tolerances
  • End preparation
  • Material Test Certificate (MTC)

The coating does not correct defects in the underlying steel pipe. For this reason, material identification and dimensional inspection should be completed before coating acceptance.


2. Check Surface Preparation

Surface preparation has a direct effect on coating adhesion. Before coating application, the steel surface should be checked for contaminants such as oil, grease, rust, mill scale, dust, and moisture. Where abrasive blasting is specified, the required cleanliness and surface profile should also be verified. For specific pipeline applications, standards define detailed requirements. For example, ISO 21809-2:2026 specifies qualification, application, inspection, testing, handling, and storage requirements for plant-applied single-layer FBE coatings used externally on bare steel pipe for pipeline transportation systems.


3. Verify the Correct Coating System

The coating must match the approved project specification and service environment. Common systems include:

Coating System

Typical Application

FBE

Pipeline and industrial corrosion protection

3PE

Buried oil, gas, and water pipelines

Epoxy

Internal or external industrial protection

Galvanizing

Construction and general outdoor applications

Inspectors should verify the coating material, application method, coating location, and specified thickness before accepting the product. The same coating should not automatically be assumed suitable for every environment. Temperature, soil conditions, moisture, chemicals, UV exposure, and mechanical damage all need to be considered.

4. Measure Coating Thickness

Coating thickness should be measured with an appropriate instrument rather than judged by appearance. Dry film thickness (DFT) inspection can determine whether the coating falls within the specified range. SSPC-PA 2 provides procedures for evaluating dry coating thickness using nondestructive gauges and includes provisions for coated steel pipe. The goal is not to make the coating as thick as possible. Both insufficient and excessive thickness can create problems, so the measured values should comply with the approved specification.

5. Check for Coating Defects and Holidays

Visual inspection should identify obvious defects such as:
  • Cracks
  • Blisters
  • Peeling
  • Scratches
  • Uneven coverage
  • Exposed steel
For coating systems where continuity testing is specified, holiday testing can help identify pinholes or other discontinuities that may not be visible during a normal visual inspection. The test method and voltage should be selected according to the coating type, thickness, applicable standard, and project specification. Holiday testing should therefore be treated as a specified inspection requirement, not a universal test for every coated steel pipe.

6. Verify Adhesion When Required

Coating thickness alone does not demonstrate coating performance. Where required by the ITP or coating specification, adhesion testing can be used to assess how well the coating remains attached to the prepared steel surface. The test method, sampling frequency, and acceptance criteria should come from the applicable specification rather than an arbitrary value selected by the inspector.

7. Review Documentation and Traceability

A professional inspection process should leave a clear documentation trail. Depending on the project, records may include:
  • Material certificates
  • Dimensional inspection reports
  • Surface preparation records
  • Coating batch information
  • DFT records
  • Holiday test results
  • Adhesion test results
  • Non-conformance reports
  • Final inspection reports
Traceability allows individual pipe batches to be linked to material and coating records, which is particularly valuable on large engineering projects.
Who Should Inspect Coated Steel Pipe?

Inspection may involve the manufacturer’s QC team, the buyer’s representative, or an independent third-party inspector. The responsible parties and inspection hold points should be defined in the purchase contract and ITP. For major projects, third-party inspection may provide an additional level of independent verification before shipment.


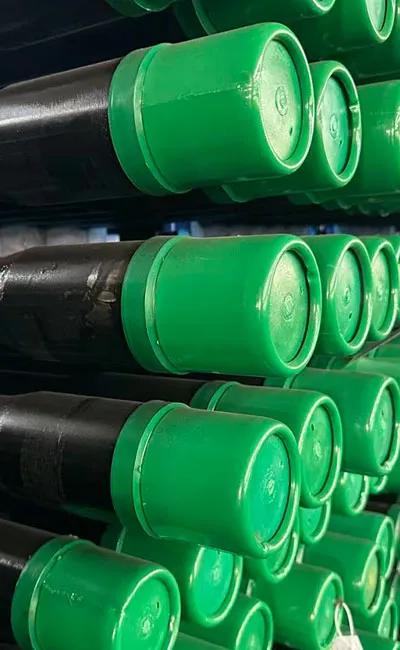
8. Inspect Packaging Before Shipment

A pipe that passes coating inspection can still be damaged during handling. Before shipment, check:
  • Pipe identification
  • Protective packaging
  • Stacking arrangement
  • Lifting method
  • Loading condition
  • Protection of coated surfaces

Dragging pipes across rough surfaces or using unsuitable lifting equipment can damage the coating before installation.


Red Flags When Buying Coated Steel Pipe

Buyers should be cautious if a supplier:
  • Cannot provide material certificates
  • Does not document coating thickness
  • Gives no clear surface preparation procedure
  • Cannot provide required inspection records
  • Has poor product traceability
  • Provides inadequate protection during transportation

A supplier’s ability to document and control the process is often as important as the appearance of the finished pipe.


Final Inspection Checklist

Inspection Stage

Key Items

Base pipe

Grade, dimensions, MTC

Surface preparation

Cleanliness, profile, contamination

Coating

Type, application, coverage

Thickness

DFT measurements

Defects

Visual and specified continuity tests

Adhesion

When required

Documentation

Reports and traceability

Packaging

Protection during shipment

Conclusion

High-quality coated steel pipe is the result of controlled pipe manufacturing, surface preparation, coating application, inspection, and handling. A reliable QA/QC process should evaluate the complete product rather than relying on visual appearance alone. Hunan Great Steel Pipe Co., Ltd. supports coated steel pipe projects with material verification, dimensional inspection, coating quality control, documentation, traceability, and export packaging. Need coated steel pipe for your next project? Send us your steel grade, dimensions, coating system, application environment, and inspection requirements for a technical review and customized supply solution.

Latest news list

  • drill pipe corrosion and washout,drill pipe washout,drill pipe erosion,drill pipe corrosion prevention,drill pipe inspection
    Drill pipe operates under repeated mechanical loads and continuous exposure to drilling fluids,abrasive solids and changing downhole conditions,Over time,these factors can contribute to corrosion,erosion and localized wall loss,In severe cases,material deterioration or mechanical damage may create a hole in the pipe body or a leak at a connection,This condition is commonly described as a drill pipe washout,Understanding the differences between corrosion,erosion and washout helps drilling teams identify potential damage and establish appropriate inspection and maintenance procedures,
  • new vs used drill pipe,drill pipe buying guide,drill pipe inspection,drill pipe procurement,drill pipe traceability
    When purchasing drill pipe,buyers often compare new and used products to balance technical requirements,availability and procurement costs,New drill pipe offers a defined manufacturing history,while used drill pipe may provide a lower initial purchase price if its condition is properly inspected and verified,However,the lowest purchase price does not necessarily represent the best value,The right choice depends on the drilling program,operating conditions,equipment compatibility and the acceptance criteria agreed before purchase,
  • drill pipe fatigue,drill pipe failure,drill string,drill pipe inspection,drill pipe cracks,rotating bending fatigue
    Drill pipe operates under repeated tensile,torsional,bending and dynamic loads throughout drilling operations,Over time,these cyclic stresses can cause fatigue damage,particularly in areas exposed to high stress or local surface defects,Unlike sudden overload failure,fatigue develops progressively,Small cracks may initiate at stress concentration points and grow with repeated loading,If the damage is not identified in time,it can eventually lead to pipe failure,drilling fluid leakage and unplanned downtime,Understanding how drill pipe fatigue develops,where damage may occur and how to inspect for potential defects helps drilling teams manage equipment reliability,
  • how to choose drill pipe,drill pipe selection guide,drill pipe size,drill pipe grades,drilling pipe procurement,drill pipe connection types
    Selecting the right drill pipe involves more than choosing a diameter and steel grade,Each specification must match the drilling program,drill string design,operating loads and connection requirements,An unsuitable selection can create compatibility problems,increase operating costs and shorten equipment service life,For drilling contractors,engineers and procurement teams,a structured selection process helps ensure that the supplied drill pipe meets both technical and project requirements,
  • drill pipe thread protection,drill pipe connection damage,tool joint threads,drill pipe make-up,thread protectors
    Drill pipe connections are exposed to repeated make-up and break-out cycles,handling impacts and demanding drilling loads,Damage to pin and box threads can affect connection reliability,increase maintenance costs and cause unplanned rig downtime,Preventing connection damage requires more than installing thread protectors,Proper handling,cleaning,thread compound application,alignment,torque control and regular inspection all contribute to longer connection service life,

Find what you need ?

close
We use cookies and other tracking technologies to improve your browsing experience on our website, to show you personalized content and targeted ads, to analyze our website traffic, and to understand where our visitors are coming from.