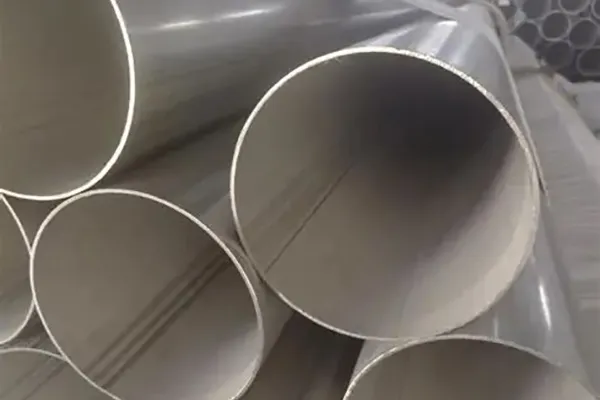

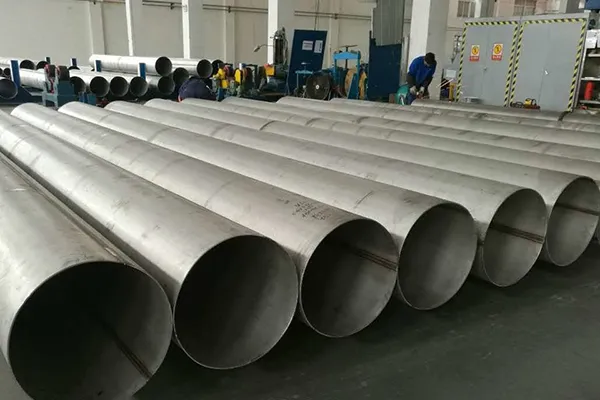
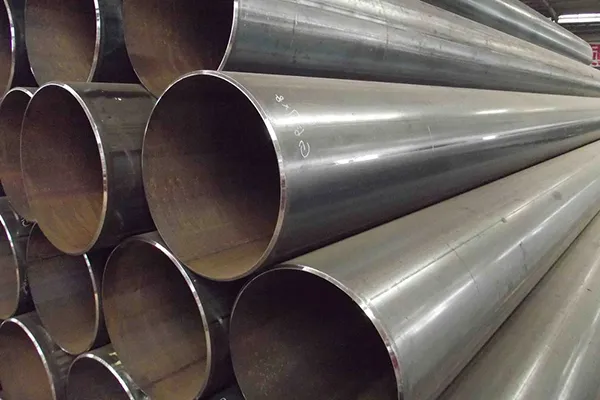
Quality control for stainless welded steel pipe should begin with the incoming material and continue through forming, welding, sizing, finishing and final inspection. For project procurement, checking only the finished pipe is not enough. A reliable inspection process should confirm that the supplied pipe matches the agreed material grade, dimensions, manufacturing requirements, testing requirements and documentation. The exact inspection plan depends on the applicable product standard and purchase specification. For example, ASTM A312 covers straight-seam welded austenitic stainless steel pipe and specifies requirements for chemical composition, mechanical properties and applicable testing.
The purpose is simple: the finished pipe should be traceable back to the material from which it was produced.
Measurements should be compared with the tolerances specified by the applicable product standard or purchase order. Generic tolerance values should not be used when the project specification defines different requirements. For larger or project-specific orders, dimensional records can also provide useful evidence during receiving inspection and fit-up.
The longitudinal weld requires particular attention because it forms part of the finished pipe wall. Inspection may include visual examination of weld appearance, alignment and surface condition. Depending on the applicable standard and purchase requirements, additional nondestructive examination may be specified. Possible methods can include eddy-current or other electrical examination, ultrasonic testing, radiographic testing or other applicable NDT methods, depending on the product and specification. Not every stainless welded pipe requires the same NDT package. For example, ASTM A312 includes requirements for nondestructive electric testing or hydrostatic testing, while additional testing may be specified through supplementary requirements.
Stainless steel pipe should also be inspected for surface condition. The inspection may look for visible defects, contamination, scratches, unacceptable weld-area conditions and other imperfections defined by the applicable specification. Surface requirements can vary significantly between general industrial, process, sanitary and decorative applications. Therefore, a purchase order should clearly state the required surface finish rather than simply specifying “stainless steel pipe.” Where surface treatment or post-weld cleaning is required, the inspection should confirm that the finished condition meets the agreed requirement.
Clear documentation allows buyers to compare the delivered pipe with the original purchase requirements and supports receiving inspection, project records and traceability.
Stainless welded steel pipe quality should not depend on one final inspection. Material verification, forming, welding, sizing, surface finishing, testing and documentation should work as one quality chain. Hunan Great Steel Pipe applies specification review and controlled inspection to stainless steel pipe orders, supporting customers in more than 80 countries with quality documentation and export coordination. Annual production is more than 2,000 tons, serving distributors, fabricators, engineering companies and industrial project buyers. For buyers, defining the inspection requirements before production is one of the simplest ways to reduce quality misunderstandings, unexpected testing requirements and receiving problems.




 English
 Español
 русский язык
 Português