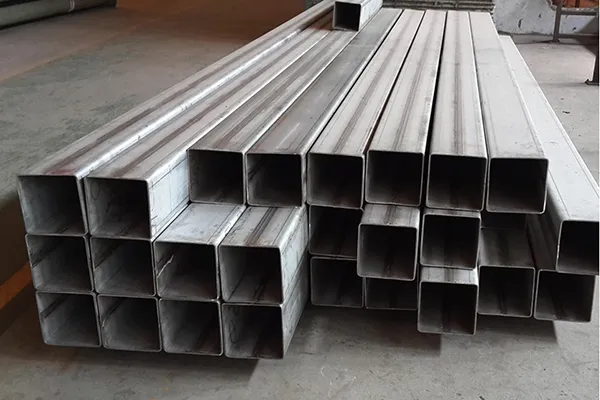
Quality control for
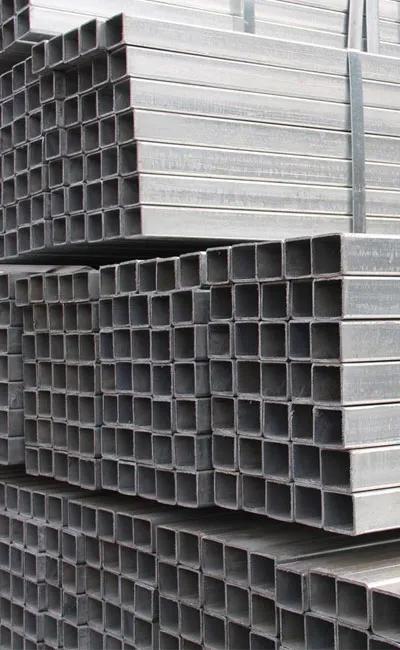
square and rectangular steel pipes involves more than checking finished dimensions. For structural applications, material traceability, dimensional accuracy, surface condition, mechanical properties, and inspection records all contribute to product conformity. For buyers sourcing square hollow sections (SHS) and rectangular hollow sections (RHS), the key question is whether the supplied products meet the purchase specification and can be verified through appropriate inspection and documentation. A reliable quality control process follows the order from material verification through production coordination, inspection, and final delivery.
Quality control starts with verifying the incoming material against the purchase requirements. Depending on the project specification, checks may include steel grade, heat number, material certificates, and other identification records. These details help establish a link between the original steel and the finished hollow section. Heat number traceability is particularly important for projects that require material verification, third-party inspection, or documented quality records. If material certificates are specified, buyers should confirm that the documents correspond to the supplied grade and relevant material identification. The required checks depend on the applicable product standard, order specification and inspection plan. Not every project requires the same level of documentation.
2. Dimensional Inspection of Hollow Sections
Dimensional accuracy affects fabrication, assembly and installation. Square and rectangular steel pipes should therefore be checked against the tolerances stated in the applicable standard or purchase specification. Typical inspection points include:
-
Outside width and height: Confirm the section dimensions.
-
Wall thickness: Check against the specified nominal thickness and permitted tolerance.
-
Length: Verify whether the supplied lengths meet the order requirements.
-
Straightness: Identify deviations that could affect fit-up or installation.
-
Corner dimensions and shape: Check section geometry where required by the specification.
-
Surface condition: Record visible imperfections that may affect use or subsequent processing.
Acceptance limits vary according to the product standard, manufacturing method, dimensions and order requirements. Buyers should avoid applying one universal tolerance to every hollow section. For projects involving multiple connected members or prefabricated steel assemblies, consistent dimensions can help reduce fitting difficulties and unnecessary site adjustments.
3. Surface and Weld Inspection
Surface inspection helps identify visible defects before the material proceeds to fabrication, coating, or installation. Depending on the product and inspection requirements, checks may cover scratches, dents, handling damage, visible cracking and other surface imperfections. For welded hollow sections, the weld area may also be examined for visible irregularities in accordance with the applicable requirements. Visual inspection has limits. It cannot replace non-destructive testing when a specification requires additional examination. The inspection method and acceptance criteria should be agreed upon before production or inspection begins. Surface condition also matters when hollow sections will receive protective coatings. Oil, moisture, rust, contaminants, or mechanical damage may affect surface preparation and coating performance. Any required surface treatment should be confirmed against the project specification.
4. Chemical Composition and Mechanical Properties
Dimensional checks alone cannot confirm that steel meets the specified material grade. Where required, chemical composition is verified against the relevant grade requirements. Mechanical testing may include tensile strength, yield strength, and elongation, as specified by the applicable standard or order. Other tests may be necessary for particular grades, applications or project requirements. Buyers should confirm which tests are required, whether testing applies to each heat or batch, and what records must be supplied. Test results should be reviewed against the specified acceptance criteria rather than assessed in isolation. The product standard, material grade, and purchase specification determine the applicable requirements.
5. Inspection Records and Export Documentation
For international steel procurement, quality records are part of order control—not simply paperwork prepared at the end. Depending on the contract, the required document package may include:
-
Material test certificates
-
Dimensional inspection records
-
Mechanical or chemical test reports
-
Visual inspection records
-
Packing lists and product identification details
-
Shipping and export documents
Before shipment, buyers should confirm the required document format, identification details, and approval process. Where third-party inspection or customer witness points are specified, these arrangements should be coordinated in advance. Clear documentation helps buyers verify the supplied material and maintain traceability throughout receiving, fabrication, and project handover.





 English
 Español
 русский язык
 Português